Choosing the best Glass Sorting Machine for recycling in 2026 is not just about finding the fastest model. A plant’s glass stream may contain clear, green, and amber fragments, plus ceramics, stones, labels, and moisture. Each contaminant can affect sorting accuracy and the quality of recovered glass. Small details matter.
A useful comparison looks at more than advertised capacity. Consider how the machine handles mixed colors, irregular glass sizes, dust, and changing feed rates. Check the sensor configuration, belt width, control options, and access for routine cleaning. Ask suppliers for test results using material similar to your own. A polished demonstration may not reflect a noisy, dusty production floor. It happens.
Operating costs deserve equal attention. Energy use, replacement parts, maintenance intervals, and operator training can shape long-term value. So can the space available for installation and the equipment already upstream or downstream. Request clear figures, but treat estimates as estimates. Even a well-designed system may need tuning after installation.
This guide introduces practical criteria for comparing glass sorting equipment and identifying a suitable option for different recycling operations. It does not assume one machine fits every plant. The best choice depends on feed composition, throughput targets, product specifications, and service support. Some details are easy to overlook. A careful trial, with representative samples and agreed performance measures, can reveal them before a purchase decision.
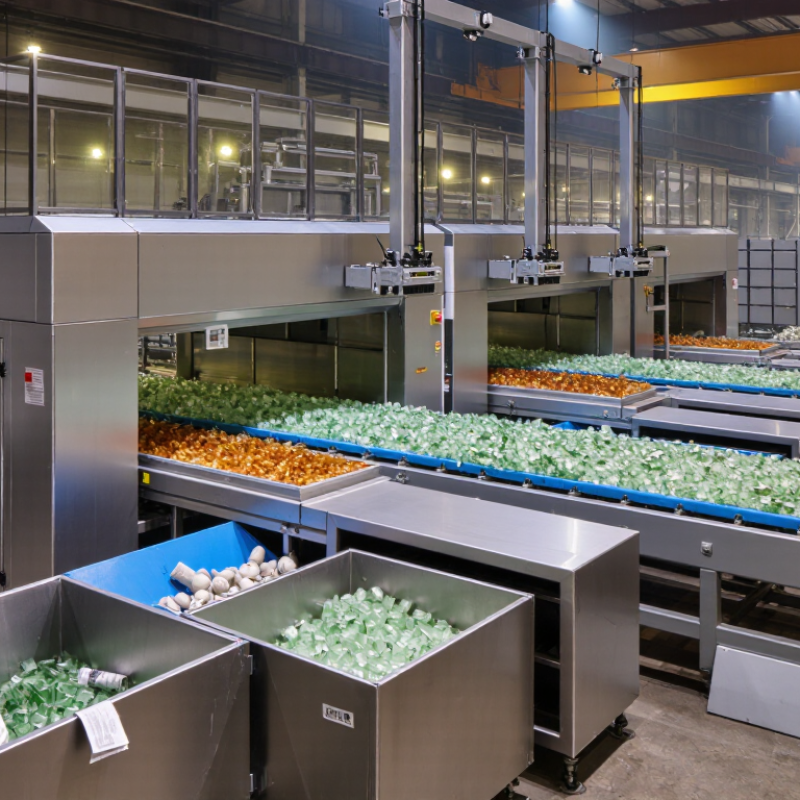
A glass sorting machine separates recovered glass by color, size, or material type. It helps recycling facilities prepare cullet, the small glass pieces used as feedstock for new products. Optical sensors inspect glass moving along a conveyor. When the system detects a target color or unwanted material, a short burst of air directs it into a separate chute. Fast, but not magic.
In a typical line, workers remove large contaminants and screens divide material by size before optical sorting. The glass should be spread in a reasonably even layer; crowded pieces can hide one another from the sensors. Operators adjust settings for the incoming mix, then check sample batches for missed ceramics, stones, or mixed-color glass. Those checks matter. A small amount of contamination can affect the quality of the recovered material.
Real plants are less tidy than diagrams. Dust, labels, moisture, and uneven glass shapes can reduce sorting accuracy, so cleaning and routine calibration are part of daily operation. Staff also monitor reject bins and adjust the feed rate when the conveyor becomes overloaded. No machine catches everything. The right setup depends on the facility’s material, throughput, and quality goals, and those conditions may change from one delivery to the next.
2026 Best Glass Sorting Machine for Recycling?
How Glass Sorting Machines Identify and Separate Materials
Glass sorting begins with a controlled feed. A vibrating screen spreads broken pieces across a moving belt, where cameras read their color, shape, and position. Some systems add near-infrared or X-ray sensors to help identify ceramics, stones, heat-resistant glass, and other contaminants. The machine then tracks each target piece and uses a brief air jet to push it into a separate chute. Small timing errors matter: one misplaced fragment can contaminate a whole batch.
The need for accurate separation is clear. The U.S. EPA’s 2018 Advancing Sustainable Materials Management report estimated that 3.1 million tons of glass were recycled from 12.3 million tons generated. Eurostat reported that the EU recycled about 75% of its glass packaging waste in 2022. These figures use different regions and measures, but both show why clean cullet matters to recycling operations.
On a real sorting line, dust, labels, wet surfaces, and overlapping shards can confuse sensors. Operators often adjust belt speed and lighting, then check rejected material by hand. Still, no sensor is infallible. A machine may mistake a clear ceramic chip for glass, or miss a tiny stone beneath a shard. Routine sampling helps reveal these blind spots, though it takes time and careful records.
| Sorting stage or method | What the sensor identifies | How material is separated | Typical feed characteristics | Best-fit recycling task | Key operating consideration |
|---|---|---|---|---|---|
| RGB color sorting | Visible color and, depending on the system, object shape or surface appearance. Common glass color categories include clear, green, and amber. | Cameras capture the material on a moving belt or chute; timed air jets eject selected pieces into a separate outlet. | Prepared, reasonably spread cullet; many systems are configured for defined particle-size bands, often in the millimetre-to-centimetre range. | Separating mixed container glass into color fractions for remelting. | Consistent illumination, a clean viewing window, and an even feed layer support reliable color recognition. |
| RGB or line-scan contaminant sorting | Visible non-glass items and visually distinct contaminants, such as some ceramics, stones, metals, plastics, or paper. | Image-processing software flags objects that differ from the accepted glass stream; air jets eject the flagged pieces. | Single-layer or well-separated material gives the camera a clearer view of individual pieces. | Removing visible foreign objects from glass cullet after screening and size preparation. | Small, obscured, or glass-like contaminants may be difficult to distinguish by visible appearance alone. |
| X-ray transmission (XRT) sorting | Differences in X-ray absorption related to material thickness, density, and composition. It can help identify certain ceramics, stones, and porcelain (CSP) in a glass stream. | The detector analyses the X-ray signal as pieces pass through the inspection zone; selected objects are rejected, commonly with air jets. | Prepared particles that pass individually through the sensing area; particle size and bed depth must suit the equipment and application. | Reducing CSP contamination where visual sorting alone is insufficient. | Performance depends on particle size, overlap, material composition, and the system’s detection settings; validate with representative feed samples. |
| Near-infrared (NIR) sorting | Spectral signatures from exposed surfaces, commonly used to distinguish many plastics and some organic materials. | The sensor classifies detectable items and directs air jets to remove selected materials from the belt or chute. | Useful when non-glass materials are present in the feed; results depend on exposed, unobstructed surfaces. | Removing certain plastics or organics from mixed recyclables before or during glass recovery. | NIR is generally not the primary method for separating glass by color or reliably identifying glass composition; dark, covered, or overlapping items can limit detection. |
| Screening and size classification | Particle size, rather than glass color or chemistry. | Vibrating or rotary screens separate material into size fractions using selected screen openings. | Mixed-size cullet; screen aperture is selected to match the process and downstream sorter. | Preparing a more uniform feed and diverting fines before optical sorting. | Screening is a feed-preparation step, not a substitute for color or contaminant identification. |
Selection note: The suitable sensor, particle-size range, throughput, and achievable product quality depend on feed composition, moisture, presentation, and the required output specification. Confirm performance through a material test and supplier-specific technical data; no single sorting method detects every contaminant.
In 2026, glass sorting lines commonly combine color cameras, near-infrared spectroscopy, and X-ray detection. Cameras classify clear, green, and amber cullet by reflected light. Air jets then eject off-color pieces. Near-infrared sensors can help identify ceramics, stones, and porcelain—contaminants that may damage furnace batches. X-ray systems detect density differences, including some opaque or heavy inclusions. No sensor sees everything.
FEVE’s 2022 industry report estimated an 80.1% glass packaging recycling rate across the European Union. The figure measures recycling performance, not cullet purity. The U.S. EPA’s 2018 materials report recorded a 31.3% recycling rate for glass containers. The years and methods differ, so these figures are not directly comparable. They do show why sorting systems must suit local material streams.
A mixed feed containing labels, wet fines, and tiny ceramic shards may need screening before optical sorting. Color cameras handle color separation; near-infrared and X-ray systems add contaminant control, but increase equipment and maintenance demands. Performance can also shift when cullet is dusty or unusually small. Manual conveyor checks remain useful, if less elegant. Plants should test with their own cullet and measure both recovery yield and ceramic carryover, rather than relying only on advertised detection rates.
A glass sorting machine should be judged on both purity and recovery. Purity measures unwanted material in the sorted glass; recovery shows how much usable glass the machine retains. Ask suppliers to test a sample resembling your actual feed, including mixed colors, labels, and small ceramic fragments. A clean demonstration sample can make almost any system look impressive. Real loads are less tidy.
Capacity figures need context. Check whether a quoted rate refers to tonnes per hour under specific conditions, not a best-case estimate. Moisture, particle size, and contamination can slow feeding or affect detection. That matters. Observe a trial over a sustained period, and record throughput alongside sorting results. One fast run proves little.
Compare the total operating cost, not just the purchase price. Include installation, energy use, routine cleaning, replacement parts, and the labor needed to manage rejects. Ask how quickly sensors can be inspected and what happens during a stoppage. Request written test conditions and maintenance assumptions. Some details may still be uncertain; your own glass stream can change by season or supplier, so budget for follow-up testing after installation.
Choosing a glass sorting machine starts with the material, not the catalogue. Sample several shifts of incoming cullet, including dusty batches, labels, ceramics, and mixed colors. Note the particle-size range and hourly throughput. Small fragments behave differently. A machine tuned for clean, uniform glass may lose accuracy when feed quality changes.
Match the sorting method to the facility’s actual targets. Optical systems can separate colors or identify contaminants, but sensor performance depends on lighting, belt loading, and calibration. Ask suppliers to test representative samples, not only hand-picked glass. Watch the reject stream. A high purity figure means little if valuable glass leaves with the rejects. Check whether the line can handle wet material and short throughput peaks.
Allow space for access, dust control, and maintenance. Operators need safe routes to inspect belts and clear routine blockages without awkward reaching. Confirm service intervals, spare-part availability, and whether settings can be adjusted by trained staff. Keep records of throughput, rejects, and downtime for several weeks after installation. Real conditions are messy. Even a well-specified machine may need tuning as feed composition shifts, and that adjustment time is easy to underestimate.